Ford Fusion: Body Repairs - General Information / Welding Precautions. General Procedures
Check
 WARNING:
Invisible ultraviolet and infrared rays emitted in welding
can injure unprotected eyes and skin. Always use protection such as a
welder's helmet with dark-colored filter lenses of the correct density.
Electric welding will produce intense radiation, therefore, filter plate
lenses of the deepest shade providing adequate visibility are
recommended. It is strongly recommended that persons working in the weld
area wear flash safety goggles. Also wear protective clothing. Failure
to follow these instructions may result in serious personal injury.
 WARNING:
Always wear protective equipment including eye protection
with side shields, and a dust mask when sanding or grinding. Failure to
follow these instructions may result in serious personal injury.
NOTICE: SRS components should always be depowered and disconnected before beginning any welding procedure.
NOTICE: Electronic modules and related wiring can be damaged when exposed to heat from welding procedures. Carefully disconnect and remove, or position away from heat affected areas.
-
A test weld should always be carried out on a test sample.
-
The correct protective clothing should always be worn.
-
Always work in a well ventilated area to avoid accumulation of noxious and oxygen displacing gases.
-
Place protective covers around components and wiring harnesses to protect from welding spatter.
-
Use grinding discs and wire brushes dedicated to the type of material being welded.
-
Follow equipment manufacturer's prescribed procedures
and equipment settings for the type of weld being used. ER70S-3 or
ER70S-6 wire is typically used for MIG welding on steel.
-
Disconnect and isolate battery ground cable.
-
Components made of Boron, Martensitic, HSS
(high-strength steel) and UHSS (ultra high-strength) steel should not be
heated to straighten or repair. Severely bent or kinked components
should be replaced with new ones.
-
Factory welds may be substituted with either STRW (squeeze-type resistance welding) spot welds or MIG plug welds.
-
MIG plug welds must equal factory welds in both location and quantity.
-
MIG plug weld holes should equal 8 mm (0.31 in) diameter.
-
Resistance spot welds must equal factory welds in quantity and be placed adjacent to original weld location.
-
Disconnect on-vehicle modules and protect them from possible heat damage and electrical currents when welding.
-
Use of a weld-through primer is recommended where applicable.
-
When welding, always place the ground clamp as close as possible to the weld area.
-
Never connect the welder ground clamp to the vehicle subframe.
-
Never weld a vehicle subframe, steering or suspension component. Service is through replacement only.


Other information:
Ford Fusion 2013–2020 Service Manual: Seatbelt Twisted at the Seatbelt Guide. General Procedures
Adjustment NOTE: Typical D-ring shown, others similar. If required, remove the necessary trim panel(s). Fold the seatbelt as indicated. Feed the folded portion of the seatbelt into the D-ring. Pull the seatbelt through the D-ring to remove the twist in the seatbelt. ..
Ford Fusion 2013–2020 Service Manual: Parameter Identification (PID) Chart. Diagnosis and Testing
Diagnostic PID Chart PID Acronym PID Name Description APP1 APP sensor 1 APP AST Time Since Start Time (in seconds) since the vehicle was started CLRDIST Distance since DTC cleared Distance driven since PCM Diagnostic Trouble Codes (DTCs) were cleared DTC PCM Continuous Co..
Categories
- Manuals Home
- 2nd Generation Ford Fusion Owners Manual
- 2nd Generation Ford Fusion Service Manual
- Body Control Module (BCM). Removal and Installation
- Pre-Collision Assist (IF EQUIPPED)
- Under Hood Overview - 1.5L EcoBoost™, 2.0L EcoBoost™, 2.5L, 2.7L EcoBoost™
- New on site
- Most important about car
Direction Indicators. Interior Lamps
Direction Indicators
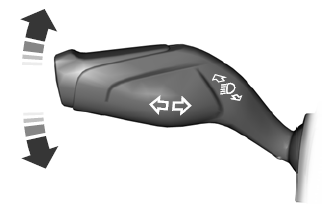
Push the lever up or down to use the direction indicators.
